A robot cell passes acceptance when it meets written, measurable requirements—not when it completes an impressive demonstration. FAT checks the integrated equipment before dispatch; SAT checks it in its installed production environment.
For an Indian factory buying its first cell, I would start with one question: what evidence must the supplier hand over before we accept the machine? This checklist turns that question into a test plan. It is an editorial planning aid, not a safety certification, legal opinion or substitute for qualified machinery-safety validation. The sample counts, durations and tolerances below are examples to negotiate, not requirements imposed by a standard.
FAT versus SAT: what changes?
| Question | Factory acceptance test: FAT | Site acceptance test: SAT |
|---|---|---|
| Where? | Integrator or equipment builder’s workshop | Final installed location |
| What does it establish? | Build matches the specification and agreed functions work before dispatch | Installed interfaces, utilities, safeguards and production process meet agreed criteria |
| What parts? | Representative parts covering the agreed variation, not only a perfect sample | Traceable production parts and model variants |
| Who operates? | Qualified integrator personnel, witnessed by the buyer | Trained site personnel under the approved test plan |
| What evidence? | Test records, drawings, software versions and open-item list | Installed validation records, production run data, training and handover records |
A successful FAT does not establish that the final installation is safe. Guard positions, nearby machines, loading arrangements and access routes can change at site. Equally, SAT should not become the first time anyone checks the basic equipment specification. Record which tests repeat after transport or software changes and who decides whether revalidation is needed.
Agree the acceptance sheet before the purchase order
Put the test protocol under revision control and reference it in the order. Define the part drawing revision, model mix, cycle start and finish, allowed operator activities, utilities, quality limits and measurement method. State who supplies parts, gauges, consumables and witnesses. A missing test coupon should not become a last-minute argument about whether a trial was meaningful.
- Throughput: distinguish robot motion time, full cell cycle and accepted parts per shift.
- Quality: identify the drawing characteristic, method, sampling plan and acceptance limit.
- Reliability: agree the observation window, downtime categories and exclusions.
- Safety: name the responsible competent people, applicable requirements and validation deliverables.
- Recovery: define permitted fault simulations and operator restart procedures.
- Handover: list as-built drawings, backups, licences, maintenance instructions, training and essential spares.
- Retesting: agree corrective-action ownership and the evidence needed to close a failed item.
A practical FAT test matrix
| Test area | Evidence to collect | Acceptance basis |
|---|---|---|
| Mechanical build | Drawing and component comparison, photographs of agreed configurations | Approved specification; deviations explicitly resolved |
| Electrical installation | Documented inspections and tests performed by qualified personnel | Applicable electrical requirements and approved design |
| Safety functions | Risk assessment, circuit information, validation results and safeguarding-distance assessment | Approved safety specification and applicable standards |
| Automatic sequence | Cycle log including stops, interventions and part IDs | Contract-agreed sequence and run criteria |
| Cycle performance | Raw timestamps, warm-up treatment, mean and agreed percentile | Agreed limits using a stated calculation method |
| Process quality | Traceable measurements with suitable calibrated equipment | Drawing or process-specific acceptance criteria |
| Controlled recovery | Results of approved fault simulations and restart checks | Safe, documented response without unexpected restart |
| Documentation | Versioned deliverable checklist and verified backup | Essential operating and safety information present before release |
Do not improvise fault tests. Deliberately jamming moving equipment, disconnecting live sensors, disturbing incoming power or bypassing interlocks can injure people and damage machinery. Use an approved, risk-assessed validation plan, manufacturer-permitted simulation methods, competent personnel and isolation where required. A safe stop alone is not proof that reset and restart behaviour are correct.
Cycle-time example: record the calculation method
The following invented dataset illustrates a contractual decision. It is not an actual robot benchmark. Nearest-rank and interpolated percentiles can produce different values on small samples, so agree the method before collecting results.
Illustrative cycle-time test
Target: 42.0 s. Permitted upper limit: target x 1.05 = 44.1 s.
Example clause: both mean and nearest-rank P95 must be <=44.1 s.

30 recorded cycles, sorted (seconds):
40.8 41.0 41.1 41.3 41.4 41.5 41.6 41.6 41.7 41.8
41.8 41.9 42.0 42.0 42.1 42.1 42.2 42.2 42.3 42.4
42.5 42.6 42.8 43.0 43.2 43.5 43.9 44.2 44.8 45.6

Sum = 1,270.9 s
Mean = 1,270.9 / 30 = 42.3633 s (0.8651% above target)
Nearest-rank P95 position = ceil(0.95 x 30) = 29
P95 = 44.8 s

Mean passes; P95 fails this example clause.
The same data passes a mean-only clause.
This sample alone does not prove sustained daily output.
Record warm-up exclusions, material changes, operator loading, micro-stops and the exact program version. If the commercial requirement is accepted parts per shift, also test that requirement directly. A percentile limit is useful only when it relates to the buyer's process; it should not be added simply to make a test look rigorous.
Quality evidence depends on the process
A resistance spot-welding cell may need qualified destructive testing and weld-monitor records; an arc-welding cell needs the inspections specified for its joint and welding procedure. A press-fit assembly may require force-displacement records and dimensional checks. A handling cell may be evaluated for surface damage and placement. Choose evidence that can detect the failure that matters.
Thirty conforming parts do not automatically demonstrate production capability. A capability study also needs a stable process, a suitable measurement system, representative sampling and an agreed statistical method. Use a small FAT sample to expose problems, and state clearly what it does not establish. Do not invent a capability target after seeing the results.
Safety validation at the installed location
Ask the integrator to identify the standards and editions used for the robot and the application. Robot product requirements and integration requirements are not interchangeable. A competent specialist must assess the complete installed system, including tooling, stored energy, access, foreseeable misuse and interfaces to adjacent equipment.
Where protective-device positioning depends on stopping performance, obtain the documented response-time and distance assessment using the applicable method. A simple “stopping distance plus reach” rule is not sufficient. Repeat relevant validation after changes to guards, sensors, loads, speeds or safety software. This article does not specify numerical safeguarding distances.
SAT, endurance runs and the open-item list
At SAT, use production-representative parts and the actual utilities. Record air pressure, supply conditions and environmental factors relevant to the process. Trained operators should demonstrate the agreed operating and recovery tasks; the integrator remains available under the supervised test arrangements.
A 72-hour endurance trial is one possible contractual choice, not a universal requirement. Choose a run length and operating pattern that can reveal the relevant wear, temperature, model-change or consumable issue. Define breaks, staffing, replenishment and planned maintenance rather than treating “continuous” as an instruction to run unsupervised.
| Example item class | Release treatment | Closure record |
|---|---|---|
| Safety or essential operating information missing | Do not release affected operation until resolved and validated | Approved corrective action and validation evidence |
| Performance requirement not achieved | Apply the agreed retest and commercial process | Repeat data against the unchanged criterion |
| Nonessential cosmetic item | May be scheduled by written agreement if it does not affect safe use or function | Responsible party, completion date and evidence |
Payment retention, rejection rights, delay damages and the effect of signing depend on the contract and applicable law. Have your legal and procurement advisers agree these provisions. Neither a signature nor a withholding percentage replaces the operator's safety obligations.
Use the integration checklist for the wider project, lead-time planning guide for dependencies, and integration-cost guide for scope. For an actual installation, engage qualified safety professionals rather than treating our standards overview as certification.
What is the difference between FAT and SAT?
FAT checks equipment at the builder before dispatch. SAT checks the installed system, site interfaces and agreed production requirements. Relevant safety validation is needed for the final installation.
Is a 72-hour SAT compulsory?
Not as a general rule stated by this article. Test duration, staffing and operating conditions must be agreed for the application and applicable requirements.
What should a cycle-time acceptance clause include?
Define the cycle boundary, included operator work, sample conditions, target, tolerance and calculation method. If using a percentile, specify how it is calculated.
Do 30 good parts prove process capability?
No. Production capability needs an appropriate study, representative sampling, a suitable measurement system and evidence of process stability.
Can I force faults to test recovery?
Only use manufacturer-permitted methods within an approved risk-assessed plan carried out by competent people. Do not improvise jams, supply disturbances or safeguard bypasses.
Sources and further reading
- ISO 10218-1:2025 catalogue entry — robot safety standard identification; consult the licensed applicable standards with your specialist.
- ISO 10218-2:2025 reference — industrial robot applications and robot cells. Catalogue identification is not evidence that this sample protocol satisfies the standard.
- ISO 12100:2010 catalogue entry — machinery risk assessment and risk reduction.
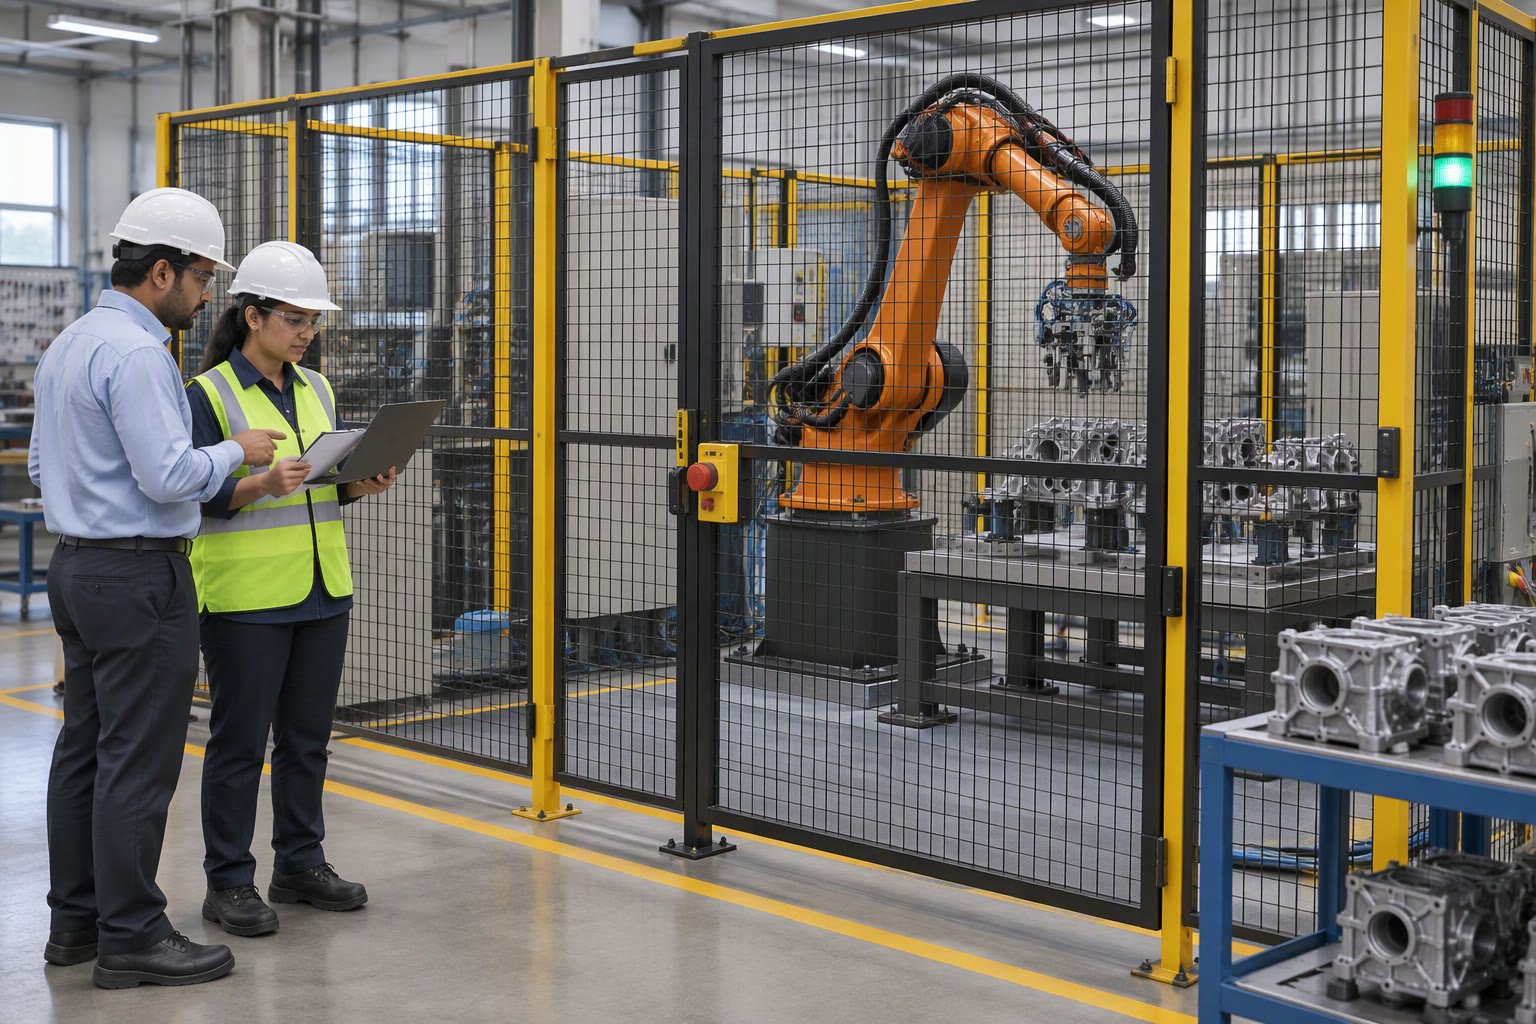
Evidence note: access to full standards text was not available for this article. The acceptance matrix is editorial guidance; the numerical dataset is synthetic. The featured image is AI-generated and does not document a tested installation.