Takt time is the available production time divided by customer demand for the same period: takt = available time / demand. It tells you how often one finished unit must leave the line to meet demand, and every station’s cycle time must be at or below it.
Key takeaways
- Takt time equals net available time divided by demand, in the same units of time per unit.
- Takt is set by customers and the shift calendar; cycle time is set by the process.
- If a station’s cycle time is longer than takt, that station is the bottleneck and the line cannot meet demand.
- Real output is lower than ideal output because of stops, so many teams compare cycle time with takt after allowing for losses.
What Takt Time Means
Takt time is the pace of production needed to match demand. The word comes from the German for a beat or rhythm, and the idea is simple: if customers want 420 units in a shift, one unit must be completed on average every so many seconds.
Takt is not how fast a machine can run. It is how fast the line must run. A machine with a faster cycle than takt will wait for work, and a machine with a slower cycle will pile up stock behind it. Takt gives every station the same target to compare against.
Available Time per Shift
Available time is the planned working time in the shift after removing planned breaks, so it is not the full clock time on the shift roster.
Subtract tea breaks, lunch, planned meetings and any planned maintenance. Do not subtract unplanned stops such as breakdowns here; those belong in a loss measure such as OEE, covered in the guide to OEE calculation in manufacturing. Work in seconds so that the final answer comes out in seconds per unit.
Worked Example
Assumptions, all placeholders: one shift is 8 hours, there are two tea breaks of 15 minutes each and one lunch break of 30 minutes, and demand is 420 units per shift.
| Step | Calculation | Result |
|---|---|---|
| Shift length | 8 h × 60 | 480 min |
| Planned breaks | 15 + 15 + 30 | 60 min |
| Available time | 480 - 60 | 420 min |
| In seconds | 420 × 60 | 25,200 s |
| Takt time | 25,200 / 420 | 60 s per unit |
Check by reversing: 60 s × 420 units = 25,200 s, which matches the available time. So this line must complete one unit every 60 seconds.
Cycle Time vs Takt
Cycle time is the time one station needs to complete its work on one unit. The line meets demand only when the slowest station’s cycle time is at or below takt.
Suppose the slowest station is a manual assembly step with a cycle time of 75 seconds. Output in the available time is 25,200 / 75 = 336 units. Demand is 420, so the shortfall is 420 - 336 = 84 units. In other words, the station is 15 seconds too slow per unit (75 - 60).
Work content matters too. If the total manual work per unit is 150 seconds, the minimum number of people or stations is 150 / 60 = 2.5, which rounds up to 3, because you cannot split a person across a fraction of a station. To measure cycle times on your own bench, the same idea of counting events over time appears in the digital tachometer with an IR sensor and LCD, where you count pulses per interval.
Adding a Robot to Close the Gap
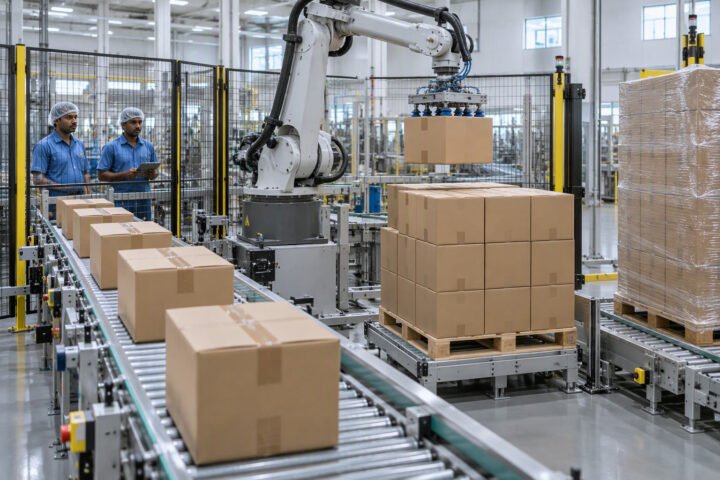
A robot can close a takt gap if its full cycle, including pick, motion, process and place, is shorter than the manual cycle. Assume, as a placeholder, that a robot cell performs the same step in 50 seconds.
- Output without losses:
25,200 / 50 = 504 units, which is504 - 420 = 84units above demand. - With losses: if the cell runs at 85 percent OEE (an assumed figure), the ideal cycle must satisfy
cycle ≤ takt × 0.85 = 60 × 0.85 = 51 s. The 50 second cycle just passes. - Check:
504 × 0.85 = 428.4units, which is above 420.
That margin is thin, so a small increase in stops would cause a miss. Estimate the robot’s time with the method in robot cycle time calculation and the plant-focused version in industrial robot cycle time calculation. To see how motion control affects cycle time at the small scale, the PID motor speed control with an encoder project shows how a controller reaches a target speed. Layout and delivery context are on the industry hub.
How to check this yourself
- Write your shift start and end times and list every planned break in minutes.
- Compute available seconds, then divide by your demand per shift to get takt.
- Time each station over at least 20 consecutive cycles with a stopwatch or a logged signal, and use the average, noting the slowest cycle as well.
- Compute
available time / station cycle timefor each station and compare with demand. - Repeat the calculation with a loss factor from your own downtime log.
Common mistakes
- Using the full 8 hours instead of net available time.
- Mixing units, for example minutes of time with units per hour.
- Using a machine’s rated speed as its cycle time instead of the measured full cycle.
- Treating takt as fixed when demand or the shift pattern changes.
- Ignoring changeover and stoppage time when checking whether a fast robot will really keep up.
Frequently asked questions
What is the takt time formula?
Takt time equals net available production time divided by customer demand over the same period. With 25,200 seconds available and 420 units needed, takt is 60 seconds per unit. Always remove planned breaks first and keep time and demand on the same basis, such as per shift.
What is the difference between takt time and cycle time?
Takt time is the pace demand requires, set by orders and available time. Cycle time is how long a station actually takes to finish one unit. For the line to meet demand, the cycle time of the slowest station must not be greater than takt time.
How many operators or robots do I need for a given takt time?
Divide total work content per unit by takt time and round up. For example, 150 seconds of work and a 60 second takt gives 2.5, so 3 people or stations. For a robot, check that its full cycle, after allowing for losses, is below takt.
Related reading
- Learn hub for more explainers on production maths.
- Tools hub for calculators to check your numbers.
- Compressed Air Consumption for Cylinders: Calculation
- Camera Field of View and Pixel Size: The Calculation
About the author and how this is kept accurate
Written, checked and maintained by Jignesh Panchal of Jaadu Digital. Figures in worked examples come from the stated assumptions, not from a bench test of our own. Read the editorial standard, follow the author on LinkedIn, or send a correction. Last reviewed: November 2026.